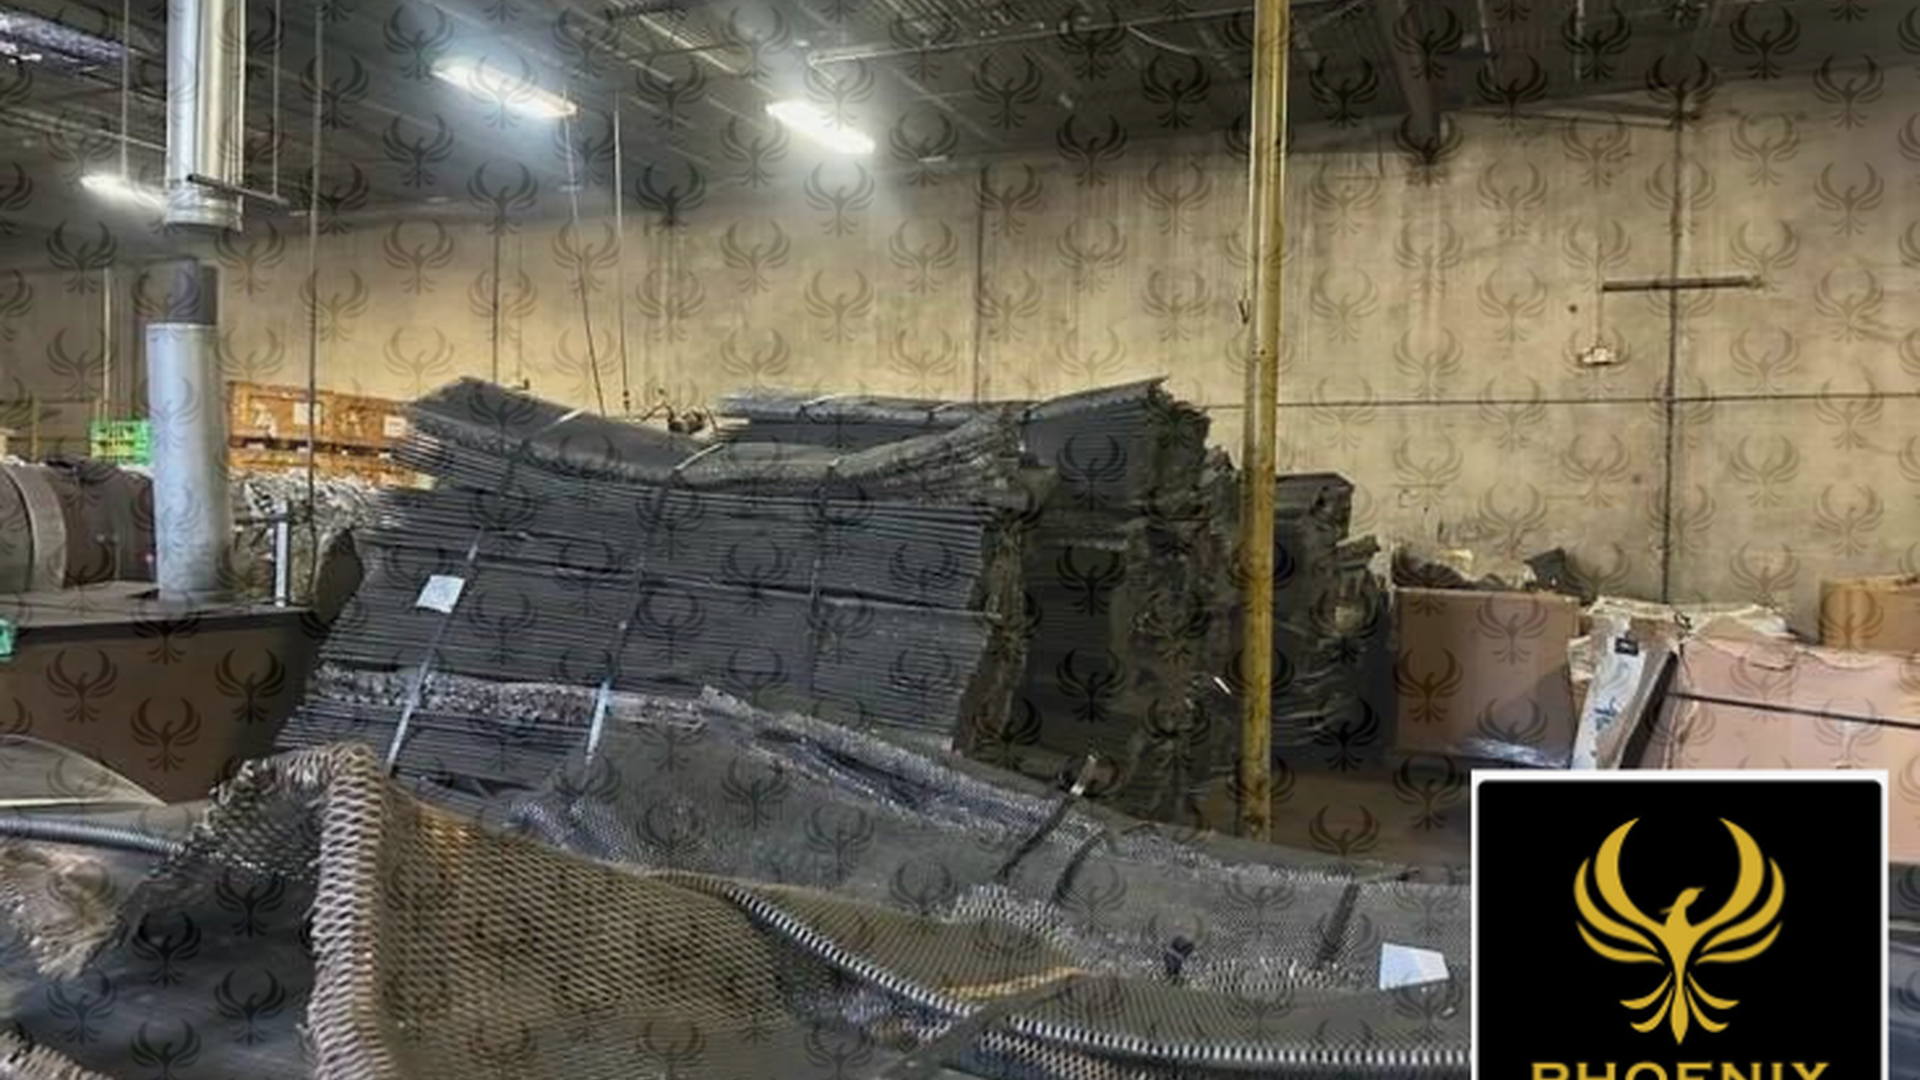
In electrochlorination, wastewater treatment, electrometallurgy, electroplating, and impressed-current cathodic protection, maintenance personnel often face a deceptively difficult question: is a black titanium mesh electrode covered with contamination, or is the black material the active catalytic coating? The distinction is critical. A healthy mixed metal oxide (MMO) titanium mesh anode is designed to be dark, rough, and non-reflective. It is not intended to look like clean, bright titanium.
The mistake typically happens when a technician sees a black, textured surface and assumes it's soot, corrosion, or fouling that must be removed. Although abrasive pads, wire brushes, scrapers, sandpaper, and acid cleaners may make the electrode appear brighter, they can also remove or weaken the catalytic layer. This often leads to permanent performance loss, higher operating voltage, and earlier electrode replacement. The opposite situation is also conceivable. Calcium scale, biological growth, oil films, and coating failure can all increase cell voltage or decrease current output. Since a single electrical measurement cannot reliably distinguish reversible fouling from irreversible catalyst loss, accurate diagnosis requires visual inspection, an understanding of the process chemistry, and conservative cleaning followed by a performance assessment.
An MMO mesh electrode consists of a titanium base with a thin ceramic catalytic coating. This coating can include ruthenium oxide, iridium oxide, tantalum oxide, titanium oxide, tin oxide, platinum, or other metal oxides. Titanium provides strength and corrosion resistance, while the coating facilitates the required electrochemical reaction, for example, chlorine evolution in brine or oxygen evolution in other process streams. A typical MMO coating is matte black, charcoal grey, or dark slate grey and is generally slightly rough, showing a fine 'mud-crack' pattern when examined closely. This texture is not a defect; it forms during manufacturing as the oxide layers are applied and then thermally cured. The microscopic cracks increase the effective surface area and help the coating withstand gas bubbles, heat, and mechanical stress during operation.
The coating should be fairly even throughout the mesh strands and should not feel greasy, slippery, chalky, or loose. One useful field test is to rub the dry mesh firmly with clean white filter paper. A well-bonded coating will not leave a visible black streak or powder. If black material transfers easily, the result could indicate loose deposits, poor coating adhesion, or coating degradation. Cleaning aims not to produce shiny silver metal; in most cases, shiny titanium indicates the active coating has been worn away, chemically attacked, or mechanically removed.
Mineral scale is an external deposit caused by water chemistry and is not part of the electrode. Common scale types include calcium carbonate, magnesium hydroxide, calcium sulfate, silica, and mixed mineral solids. This type of deposit is particularly common in areas with hard water, warm systems, high pH, low flow rates, and cells with insufficient circulation.
Scale tends to form on the cathodes because hydrogen evolution increases the local pH at the electrode surface. Even if the overall water chemistry appears acceptable, the boundary layer adjacent to the cathode can become alkaline enough to precipitate calcium and magnesium. In cells that use polarity reversal, the scale can also develop on an electrode that periodically functions cathodically.
Calcareous scale is generally white, off-white, light tan, or beige; it is usually chalky and brittle, forms a crust, and may span the openings of the diamond-shaped mesh. As it builds up, it obstructs flow, reduces active surface area, and gradually raises cell voltage. Some mineral deposits are dark-colored. In an industrial electrolyte that contains manganese, dark brown or black manganese dioxide may build up on the anodes. However, unlike a factory-applied MMO coating, manganese deposits are usually uneven, patchy, fibrous, or clustered. A proper coating is generally incorporated into the mesh surface, whereas fouling tends to hide the original surface texture or gather in separate areas.
Biofouling and organic contamination are usually more deceptive than mineral scale since they can be very thin. Wastewater, seawater, cooling water, and industrial process fluids may contain microorganisms, oils, greases, siloxanes, and other organic compounds. These substances can result in a translucent film, a slimy biological layer, a brownish or greenish deposit, or an almost invisible hydrophobic surface film.
Although organic films may be much thinner than mineral scale, they can cause a greater electrical penalty. Oils, grease, and biological polymers can form continuous insulating barriers that prevent proper contact between the electrolyte and the catalytic surface. As a result, an electrode may show a sharp voltage increase even when it appears visually clean. A water-sheet test can detect organic contamination. When you rinse a clean electrode surface with new demineralized water, the water should spread out evenly. However, if the water beads up, pulls off, or leaves dry-looking areas, this may indicate a hydrophobic oil or organic film. Biofouling is especially common when the system is shut down, during intermittent operation, in stagnant conditions, and at low current levels.
The worst case is not normal fouling, but the titanium substrate becomes exposed after the catalytic coating is damaged or used up. Although titanium normally forms a thin oxide layer, it can develop into an insulating barrier under anodic conditions. This phenomenon, called passivation, hinders electron transfer and can cause a large rise in cell voltage. Passivated titanium can look different from both the scale and a typical coating; it may appear silver-gray or metallic because the black coating has vanished, and it can also show rainbow interference colors such as bronze, purple, blue, gold, pink, teal, or green. These colors indicate oxide-film formation on titanium and are not normal on an intact MMO surface.
In the most serious cases, localized electrical stress may cause powdery white titanium dioxide spots from micro-arcing or dielectric breakdown. The spots can be confused with calcium scale; however, if white spots appear with rainbow coloration, if exposed titanium is present, or if high operating voltage is maintained continuously, the electrode may suffer permanent damage rather than just becoming fouled.
MMO electrode maintenance should follow one fundamental principle: soak and flush, not scrape and strip. When dealing with mineral scale, use a manufacturer-approved chelating cleaner that is neutral or only slightly alkaline, such as sodium EDTA, GLDA, NTA, polyaspartic acid, or buffered sodium citrate, as appropriate. These products bind calcium and magnesium ions and slowly dissolve deposits without exposing the coating to strong acid.
Clean biofilms and organic matter with neutral enzymatic cleaners or gentle detergents. If you cannot clean an electrode right away, keep it submerged in clean demineralized water so biological deposits do not dry out and harden on the surface. Oils and grease may require treatment with a suitable solvent, then thorough rinsing.
After soaking, remove deposits with a soft sponge, a soft-bristled brush, or by rinsing with low- to moderate-pressure water. When working with the electrode, wear clean gloves, as skin oils may affect surface wetting.
Do not use abrasive cleaning on MMO-coated mesh, as wire brushes, metal scrapers, abrasive pads, sandpaper, pumice, and grit blasting will remove the thin ceramic catalyst and expose the titanium substrate. When the titanium is exposed, passivation can begin, and current will shift to the still-coated areas, accelerating electrode failure.
Avoid acid cleaning unless the electrode manufacturer has approved a documented procedure. Hydrochloric, sulfuric, phosphoric, and hydrofluoric acids can dissolve coating components, seep into microscopic cracks, and attack the titanium-coating interface. Fluoride cleaners are especially hazardous because they can attack both titanium oxide and titanium metal, leading to rapid coating loss.
A black titanium mesh isn't necessarily dirty; in numerous systems, the matte-black surface acts as the active MMO catalyst and enables the electrode to function. White crusts usually indicate mineral scale, while slippery or water-repelling surfaces suggest biofouling or organic films. Silver spots or rainbow colors indicate possible coating loss and titanium passivation.
Accurate identification prevents harmful maintenance; operators should use cleaning methods that are neither abrasive nor acidic when dealing with removable deposits and know how to tell whether visual signs indicate irreversible electrode damage. By preserving the catalytic coating, operators can extend the electrode's life, stabilize the operating voltage, and keep the titanium mesh suitable for recoating instead of replacement.